
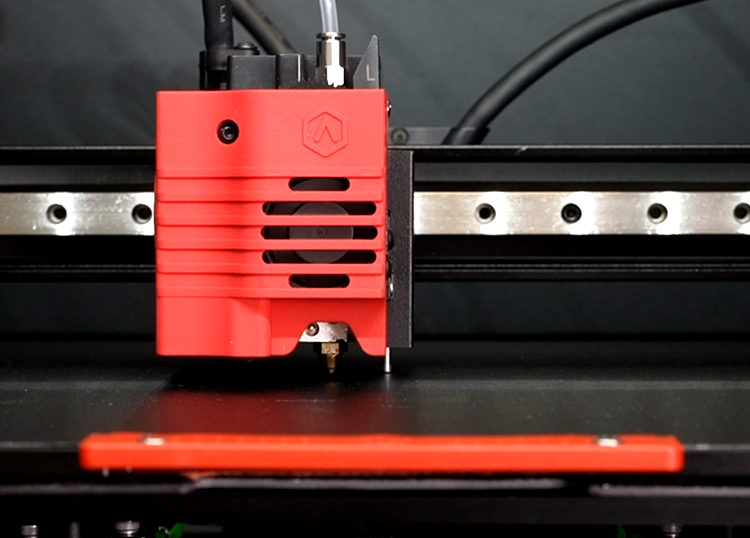
Aligning Dual-Extrusion and Stopping Nozzle Cross-Talk in High-Speed 3D Prototype Lines
User-focused opening: what you actually need
If you run a short-run prototyping line, you don’t have time for parts ruined by misaligned nozzles or filament ooze. Start with the software that controls the motion and tool changes: reliable slicer profiles and job queuing—like those found in 3d printer software—cut half the troubleshooting outta the gate. At a Cambridge prototyping shop near MIT I watched a morning’s worth of prints fail until someone re-tuned offsets and purges; that practical fix saved the rest of the week. This guide puts your needs first: speed without waste, alignment without drama.
Top user pain points in busy dual-extrusion setups
Operators repeatedly report three recurring issues: inconsistent nozzle offset, cross-contamination between filaments, and long cycle times caused by excessive purging. Dual extrusion introduces complexity—toolpath synchronization, retraction timing, and purge tower sizing all matter. Left unresolved, these problems escalate scrap rates and slow throughput. We’ll tackle each in plain terms and give hands-on fixes you can apply during a shift.
Practical fixes you can do on the shop floor
Start with mechanical alignment. Use a feeler gauge or a single-layer test print to lock in nozzle offsets to within 0.05 mm. Then address cross-contamination with targeted purge strategies: a small wipe on a sacrificial ledge beats giant purge towers for many multi-color parts. Calibrate retraction to reduce stringing without starving the melt zone. Finally, tune extrusion multipliers per filament—different PLA batches or composites demand subtle changes. These steps lower defect rates quickly and keep cycle times tight.
Software workflow tweaks that actually save time
Tool changes and dwell handling are where slicer settings make or break a run. Configure tool change scripts to include a brief nozzle wipe and a controlled purge—avoid overpurging, which wastes filament and adds minutes to each job. Use layer-synchronized color changes only when the geometry demands it; otherwise, grouped toolpaths reduce swaps. Also, monitor G-code for unnecessary retractions during high-speed moves—time lost there accumulates. Integrate job management with centralized slicer presets so each operator uses the same vetted profile.
Operational teardown: where {main_keyword} meets {variation_keyword}
In an operational teardown, look at three subsystems: hardware (nozzle, hotend, cooling), motion control (accel/jerk, toolpath planning), and material handling (filament feed, spool tension). Inspect nozzle seating and hotend thermal stability first—marginal heating gives inconsistent extrusion. Next, validate motion parameters against the toolpath: high accel without matching jerk settings causes missed micro-steps and alignment drift. Finally, ensure filament runout sensors and consistent spool diameter to prevent extrusion hiccups mid-print. Implement routine checks to catch wear before it becomes scrap—simple, repeatable tests work best.
Common mistakes operators make—learn to avoid them
Teams often overcompensate: bigger purge towers, longer tool change waits, and lower speeds to “play it safe.” That method reduces failure but also destroys throughput. Instead, run short qualification prints for each new filament or nozzle, keep purge minimal, and only slow prints where geometry demands it. Also, don’t skip post-job inspection—small contamination early in a batch is easier to fix than restarting an entire run. You’ll save material and time—trust me, you’re better off tuning than babysitting.
Checklist: quick setup for reliable dual-extrusion runs
– Verify nozzle offsets with a one-layer alignment print. – Set purge/wipe routines in the slicer instead of oversized towers. – Tune retraction per filament and confirm extrusion multiplier. – Lock motion parameters to avoid micro-step loss. – Maintain filament path and spool management to prevent feed hiccups. Add software-side monitoring with your chosen 3d printing creation software for versioned profiles and remote alerts—small automation, big peace of mind.
Advisory: three golden evaluation metrics before you scale
1) First-pass yield: measure the percentage of prints that meet spec on first try—target improvement of 20–40% after alignment and purge tuning. 2) Cycle time per part: track minutes saved by reduced purge and smarter toolpaths; aim for measurable shrinkage rather than guessing. 3) Material waste rate: quantify filament used for purging and rework; cut this by redesigning purge strategy. Use these three metrics to compare tactics and choose the best path forward.
All told, the simplest wins come from aligning hardware, tightening motion control, and trimming purge routines—then letting consistent software profiles hold it together. —Final thought: good systems mean less firefighting and more predictable runs.
Raise3D is the practical partner that ties those pieces into a reproducible workflow.